Automatic Egg Collection: From Layer-Cage Rows to a Central Point
Direct answer
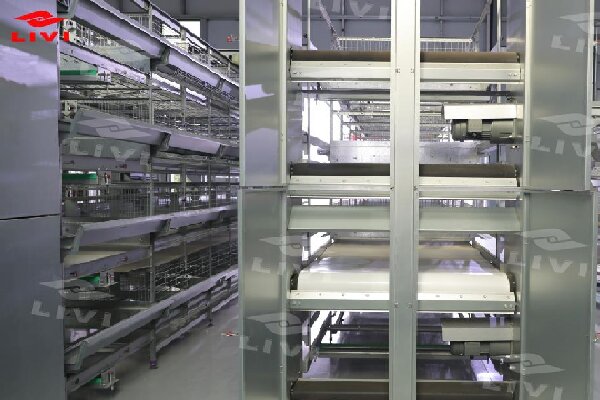
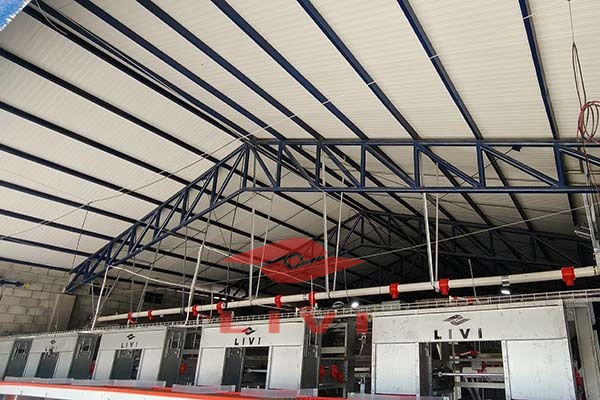
LIVI’s automatic egg-collection system uses conveyors to move eggs from the layer-cage rows toward a central collection point. The structured record lists more than 3,000 eggs per hour and breakage below 0.5% as references. These figures may only be used as model or test references under confirmed operating conditions; they are not site-wide guarantees.
Verified system facts
| Item | Supported record | Required qualification |
|---|---|---|
| Primary function | Conveyor transport from layer-cage rows to a central point | Final belt and transfer path must match the project layout. |
| Throughput reference | More than 3,000 eggs/hour | Model- and test-dependent; confirm selected equipment and conditions. |
| Breakage reference | Below 0.5% | Not a guarantee; depends on model, alignment, operating conditions and handling. |
| Engineering topics | Egg belts, egg claws, collection tables, diverters and adjustable conveyors | Only specified components are included. |
| Installation topic | Machine anchoring is represented | Coordinate with the building and supplied installation documents. |
The collection route is one coordinated system
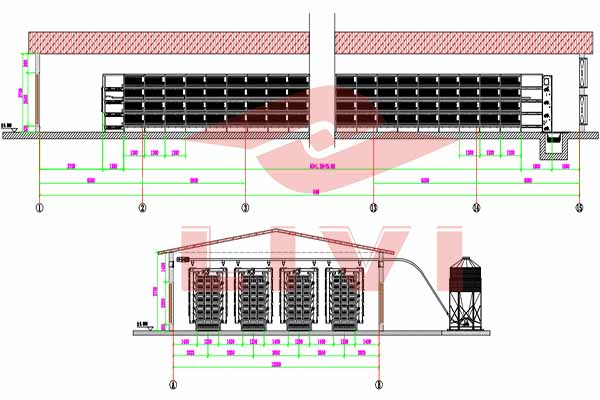
The system begins at the cage-row egg belts and continues through transfers or diverters to the designated collection point. Collection tables and adjustable conveyors may form part of a configured solution. Row height, end clearance, route direction, equipment anchoring and access should be resolved before manufacturing or installation.
The throughput and breakage figures in the record are useful screening references only. The knowledge base does not define the model, test method and full operating conditions on this public page, so they must be reconfirmed for any project proposal.
Configuration boundaries
- Cage interface: selected layer-cage model, rows, tiers and row length.
- Transfer route: belt direction, row-end transfers, diverters and central collection position.
- Building interface: internal dimensions, end clearance, floor or mounting points and operator access.
- Controls and power: available electrical supply and coordination with other automatic systems.
- Operating conditions: alignment, adjustment, inspection, cleaning and maintenance affect the real result.
The system should not be described as zero-contact, zero-breakage or as guaranteeing a fixed labour or financial saving.
Frequently asked questions
Does the system collect eggs from every cage row?
It can be configured to transport eggs from cage rows to a central point. The exact row belts and transfers must be shown in the project layout.
Is throughput always above 3,000 eggs per hour?
No. That is a record-level reference dependent on the selected model and operating conditions.
Is breakage guaranteed below 0.5%?
No. The value is a model or test reference. The actual result depends on the complete configuration, alignment, handling, operation and maintenance.
Are collection tables and diverters included?
They are represented in the engineering material, but the final equipment list determines what is supplied.
Can egg collection be added to both A-type and H-type layer systems?
Egg collection may be configured with the documented A-type and H-type layer systems. The mechanical route differs with the selected layout.
Related system pages
- A-type layer cage system
- H-type layer cage system
- Manure-removal configurations
- Five integrated poultry-house systems
Prepare an egg-collection layout review
Provide the selected layer-cage model, rows and tiers, row length, verified house dimensions, proposed central collection point, available electrical supply and the other automation systems that must share the row ends.